
High Performance Tundish Dry Vibration Material China Suppliers and Factory
CONTACT
NOW DOWNLOAD PDF
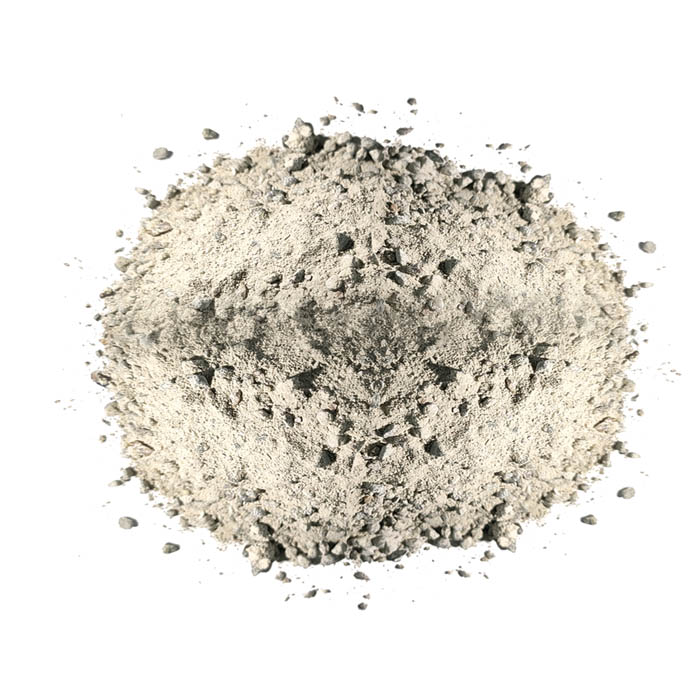
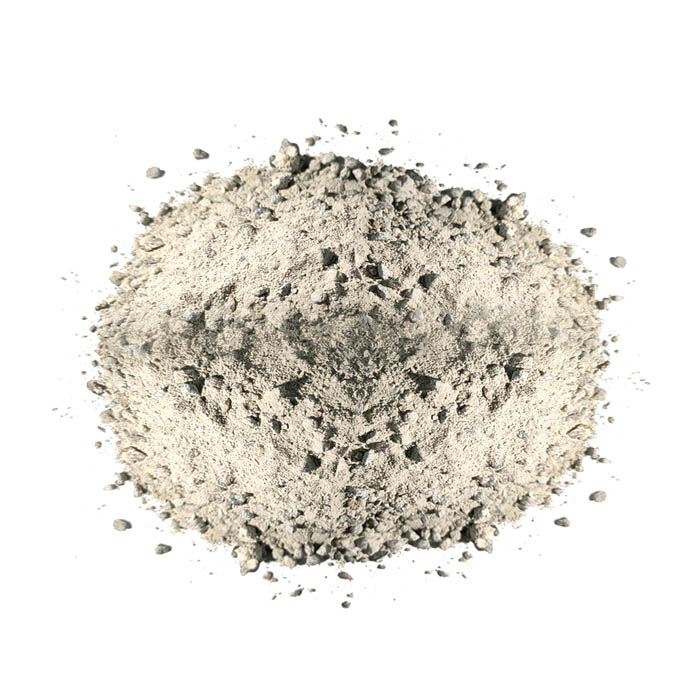
Our Tundish Dry Vibration Material is a high-performance refractory solution engineered specifically for the demanding environment of continuous casting. Designed to optimize the interface between the permanent lining and the tundish shell, this material ensures superior thermal insulation and structural stability, significantly reducing labor intensity through a simplified installation process.
By integrating advanced magnesia and siliceous compositions, our dry vibration material facilitates extended continuous casting cycles exceeding 35 hours. It is meticulously formulated to prevent liquid steel contamination, enhance billet quality, and reduce energy consumption during the baking process, making it an essential choice for modern steel plants seeking operational efficiency and cost reduction.
Detailed Parameters
| Material Type | Magnesia Vibrating Material | MgO Content | ≥75% |
|---|---|---|---|
| SiO2 Content | ≤2.5% | Bulk Density | ≥5.0 g/cm³ |
| Withstand Pressure | -0.2 to 0 MPa (250℃ x 3h) | Linear Change | 0% (1500℃ x 3h) |
| Alternative Type | Magnesium Siliceous Material | MgO Content (Siliceous) | ≥60% |
| SiO2 Content (Siliceous) | ≥20% | Bulk Density (Siliceous) | ≤2.5 g/cm³ |
Key Advantages
Superior Erosion Resistance
Engineered to withstand harsh molten steel environments, ensuring structural integrity and reducing tundish slagging rates.
Extended Service Life
Achieves continuous casting times exceeding 35 hours, significantly increasing production uptime and efficiency.
Enhanced Steel Purity
Low slagging rates help purify liquid steel, directly improving the chemical quality and surface of the steel billets.
Energy Efficiency
Shortened baking times and high thermal efficiency lead to significant energy savings during pre-heating phases.
Easy Decoating
Designed for effortless flipping and removal after use, reducing maintenance time and operational costs.
Non-Toxic & Safe
Environmentally friendly, non-toxic composition ensuring a safer working environment for plant operators.
Product Gallery
Management Platforms
Installation Prep
Place metal membrane in tundish with a precise working gap of 5-12cm from the permanent lining.
Filling Process
Manually pour dry vibration material into the gap and vibrate the membrane to achieve maximum density.
Membrane Heating
Heat within the membrane at 250°C-400°C for 1-2 hours using a specialized heater.
Membrane Removal
Carefully lift and remove the membrane only after the system has completely cooled down.
Final Baking
Bake on medium-low heat for 1 hour, followed by high-heat red baking before pouring steel.
Thermal Control
Ensure tundish walls remain hot after red baking to prevent loose cladding and guarantee performance.
Investment Return Comparison
| Performance Metric | Standard Material | Our Dry Vibration Material |
|---|---|---|
| Casting Duration | Typical Cycle | Over 35 Hours |
| Energy Consumption | Standard Baking | Low (Short Baking Time) |
| Labor Intensity | High/Manual | Reduced (Simple Construction) |
| Steel Quality | Standard Purity | Enhanced (Low Slagging Rate) |
| Maintenance Cost | Higher Decoating Effort | Lower (Easy Flipping) |
Frequently Asked Questions
Q: What is the primary purpose of Tundish Dry Vibration Material?
It acts as a high-efficiency refractory layer that provides thermal insulation, protects the tundish shell, and ensures the purity of liquid steel during continuous casting.
Q: How does this material improve steel billet quality?
By maintaining a low tundish slagging rate, it minimizes impurities in the liquid steel, resulting in higher purity and better quality steel billets.
Q: What are the recommended packaging options for shipment?
We offer 1-ton Jumbo Bags, 10kg small bags within Jumbo Bags, 25kg small bags within Jumbo Bags, or customized packaging as per request.
Q: Why is it important not to cool the tundish wall after red baking?
Keeping the wall hot prevents the cladding structure from loosening, which is critical for maintaining the material's performance and structural integrity.
Q: Which delivery ports are available for international shipping?
Our products are primarily shipped through Xingang Port or Qingdao Port, China.
Q: How does the service life of this material compare to industry standards?
With an average service life of over 35 hours, our material reaches an advanced level in the industry and is highly recognized by major steel plants.